
 HOTLINE:+8613974960765 +8618507312158 HOTLINE:+8613974960765 +8618507312158


— Knowledge —
— PRODUCTS —
 Service Hotline +8613974960765
Email:susie@hnljpump.com
Mobile:+8618507312158
TEL:+8613974960765
Right Angle Gearboxes
Publication date:2025/5/30 0:08:26 popularity: [content:visits]
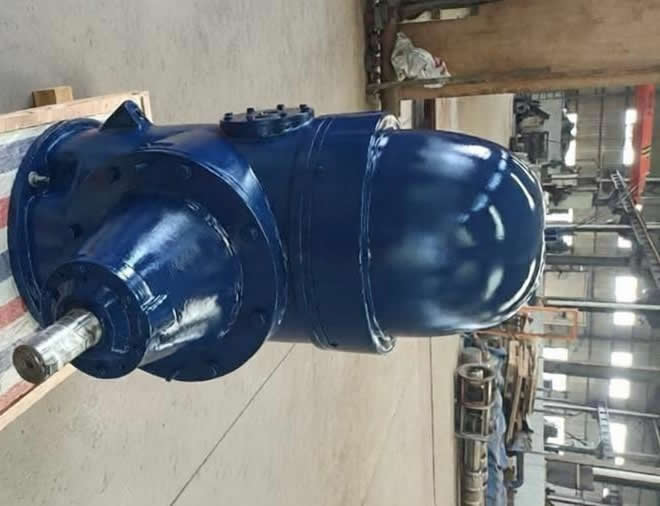
This case study focuses on the condensate system renovation project of a 600MW supercritical thermal power unit. The H-series right angle gearbox is used to achieve 90 ° right angle transmission between the steam turbine and the vertical condensate pump, solving the core pain points of space limitation and axial thrust overload in traditional direct drive, and achieving energy saving, efficiency improvement, and long-term stable operation of the unit.
🏭 Project background and original pain points
The original 600MW unit condensate water system of the power plant adopted a conventional motor direct drive vertical condensate water pump scheme, which exposed multiple core problems that could not be solved during operation:
The spatial layout is severely limited: the vertical motor is directly stacked above the pump body, and the total axial height of the unit exceeds 3.2m. The floor height of the underground condensate water pump room is only 3.8m, and the daily operation and maintenance lifting space is seriously insufficient. Conventional cranes cannot be used for disassembly and maintenance, and a single maintenance takes more than 48 hours, seriously affecting the efficiency of unit start stop.
Frequent axial thrust overload: The rated flow rate of the condensate pump is 1200m ³/h and the head is 320m. The maximum axial thrust generated during operation is 98000N. The original vertical motor has a thrust bearing with a rated load of only 60000N. On average, bearing burnout occurs after 6 months of long-term overload operation, and the risk of unplanned shutdown is extremely high.
High operating energy consumption: The original motor direct connection scheme cannot adapt to the rated speed of the small steam turbine, and an additional hydraulic coupling must be installed for speed regulation. The transmission loss is as high as 15%, and the annual power consumption of a single pump in the condensate system exceeds 4.2 million kWh, resulting in a high plant power consumption rate.
Damaged components due to start stop impact: During the start stop of the unit, the pressure fluctuation of the condensate system is large, and the instantaneous axial impact load exceeds 110000N. There are frequent occurrences of pump shaft movement exceeding the standard and mechanical seal leakage faults. On average, the unit is shut down for maintenance more than 3 times a year due to seal leakage.
🛠️ Customized selection scheme for H-series right angle gearbox
For the working conditions of this project, a customized upgraded H-series right angle gearbox is selected, with a core configuration that fully matches the special requirements of the turbine driven condensate system:
Accurate matching of core parameters:
Adapt to a small steam turbine with an input power of 1250HP (approximately 920kW), with 20% power redundancy reserved. The rated input speed is 3000rpm, and the pump output speed is 2500rpm through a customized transmission ratio of 1.2:1, fully matching the rated operating point of the condensate pump. Cancel the original hydraulic coupling structure.
Upgraded heavy-duty thrust roller bearings, with a rated axial thrust bearing capacity of 125000N, fully covering the maximum axial thrust of 98000N during pump operation, and reserving 27% of thrust redundancy, completely solving the problem of overload of the original motor bearings.
Targeted optimization of structure:
Adopting 20CrMnTi alloy steel carburizing and quenching gears, the accuracy has been upgraded to level 6, the meshing backlash is controlled at 0.15~0.2mm, and the transmission efficiency reaches 97.5%, far higher than the original hydraulic coupler's 85% transmission efficiency.
Equipped with an independent forced oil injection lubrication and circulating water cooling system, the oil temperature can be stably controlled below 55 ℃. The shaft end is sealed with fluorine rubber double lips, with a protection level of IP55, suitable for the special environment of high humidity and high steam in the pump room.
Installation layout optimization:
The small steam turbine is horizontally arranged on the ground floor of the pump room, and drives the vertical condensate water pump by turning 90 ° through the H-series right angle gearbox. The total axial height of the unit is reduced from 3.2m to 1.8m, completely solving the problem of insufficient lifting space in the underground pump room.
The coaxiality error between the right angle gearbox, turbine, and condensate pump is controlled within 0.08mm, and a high-precision elastic coupling is used to fully absorb the shaft system impact vibration during start stop moments.
✅ Actual testing effect of project implementation
After the renovation project was put into operation, it operated continuously for 36 months without any faults, and its performance indicators far exceeded expectations
Significant energy-saving benefits: After the cancellation of the hydraulic coupling, the system transmission loss decreased from 15% to 2.5%, and a single condensate pump saved 3.2 million kWh of electricity annually. Calculated based on the power plant's on grid electricity price of 0.35 yuan/kWh, the annual direct increase in revenue exceeded 1.12 million yuan, and the entire renovation cost can be recovered in 18 months.
Significant improvement in reliability: The heavy-duty thrust bearing of the right angle gearbox fully supports all axial loads of the pump, and the shaft vibration value remains stable below 2.6mm/s, completely eliminating the original motor thrust bearing burnout fault. The continuous fault free operation time of the equipment has been extended from 6 months to 36 months, and the reliability of the condensate system has been improved to 99.9%.
Doubling operation and maintenance efficiency: After the total height of the unit is significantly reduced, daily maintenance can be directly carried out using the conventional crane in the pump room for lifting. The dismantling and maintenance time of a single pump body has been reduced from 48 hours to 8 hours, greatly reducing the waiting time for unit start stop and reducing unplanned downtime losses by more than 2 million yuan per year.
Enhanced adaptability to working conditions: Through precise matching of the transmission ratio of the right angle gearbox, the condensate water pump always operates in an efficient working range when the load of the unit varies from 30% to 100%. The vacuum degree of the condenser is steadily increased by 0.7kPa, and the overall power generation efficiency of the unit is improved by 0.45%.
📌 Summary of core project experience
When selecting the condensate water system driven by a steam turbine, the maximum axial thrust of the pump must be taken as the core selection basis. It is forbidden to directly choose a common right angle gearbox with the same power. A customized H-series right angle gearbox model with upgraded high thrust bearing must be selected, with more than 25% axial thrust redundancy reserved.
In the scenario of high-power steam turbine drive, an independent forced lubrication and cooling system must be equipped, and the use of basic splash lubrication structure is prohibited to avoid early pitting and wear caused by insufficient lubrication of the tooth surface during high-speed operation.
The right angle gearbox scheme can be directly replicated and promoted for the condensate water system renovation of 300MW~1000MW full capacity thermal power units, which is the mainstream technology route for cost reduction, efficiency improvement, and power consumption reduction in current power plants.
Project Background:
A certain power plant has ordered multiple vertical multi-stage drum bag type condensate pumps (small machine condensate pumps), matched with H-series right angle gearboxes, for the condensate water system driven by steam turbines.
Technical points:
·Pump type: Vertical multi-stage drum bag type (JLTDN series)
·Supporting: H-series right angle gearbox (90 ° steering)
·Power source: small steam turbine (horizontal output)
·Key requirement: Under high-temperature condensed water conditions, it is necessary to withstand the large axial force (≤ 125000N) generated by the self weight of the water pump
Analysis:
The condensate pump is a critical auxiliary equipment in power plants and requires continuous high reliability operation.
The core value of a right angle gearbox here lies in:
① converting the power of a horizontal small steam turbine into a vertical shaft driven deep well pump;
② Directly bearing the huge axial thrust generated by multi-stage impellers, avoiding the need for additional thrust bearings on the pump body, and simplifying the pump body structure;
③ Easy to disassemble and assemble the drive end separately during maintenance.
Previous:Case study of H-series right angle gearbox for condensate water system driven by steam turbine
Next:没有了!
Related Recommendations

Service hotline
screenshots ,WeChat Scan the Qr Code
WeChat:ljpump6666